- Home
- Request for Quote
- Products
- Variable Frequency Drive Systems and Controls
- AC Variable Frequency Drives
- ABB ACS150 Component Drives :: Overview
- ABB ACS150 Component Drives :: Technical Specifications
- ABB ACS150 Component Drives :: Ratings, Types, Voltages and Construction – Prices
- ABB ACS150 Component Drives :: Dimensions, Weight and Noise
- ABB ACS150 Component Drives :: Interface and Options (prices)
- ABB ACS150 Component Drives :: Technical Data
- ABB ACS150 Component Drives :: Control Connections
- ABB ACS350 General Machinery Drives :: Overview
- ABB ACS350 General Machinery Drives :: Technical Specifications
- ABB ACS350 General Machinery Drives :: Ratings, Types, Voltages and Construction
- ABB ACS350 General Machinery Drives :: Dimensions, Weight and Noise
- ABB ACS350 General Machinery Drives :: Interface and Options (prices)
- ABB ACS350 General Machinery Drives :: Technical Data
- ABB ACS350 General Machinery Drives :: Control Connections
- ABB ACS550 AC Variable Frequency Drive :: Overview
- ABB ACS550 AC Variable Frequency Drive :: Hardware Description
- ABB ACS550 AC Variable Frequency Drive :: Standard Features and Options
- ABB ACS550 AC Variable Frequency Drive :: Specifications
- ABB ACS550 AC Variable Frequency Drive :: 230V Ratings (pricing)
- ABB ACS550 AC Variable Frequency Drive :: 380V Ratings (pricing)
- ABB ACS550 AC Variable Frequency Drive :: 480V Ratings (pricing)
- ABB ACS550 AC Variable Frequency Drive :: Dimensions: ACS550 NEMA 1 R1 through R6 Frame Size
- ABB ACS550 AC Variable Frequency Drive :: Dimensions: ACS550 NEMA 12 R1 through R6 Frame Size
- ABB ACS550 AC Variable Frequency Drive :: Dimensions: ACS550-02 NEMA 1 R7 Frame Size
- ABB ACS550 AC Variable Frequency Drive :: Dimensions: ACS550-02 NEMA 1 R8 Frame Size
- ABB ACS550 AC Variable Frequency Drive :: Dimensions: ACS550-U2 NEMA 1 R7 & R8 Frame Size
- ABB ACS 600 Adjustable Speed AC Drives
- ABB ACS800 AC Variable Frequency Drive :: Overview
- ABB ACS800 AC Variable Frequency Drive :: Standard Features / Available Options and Software
- ABB ACS800 AC Variable Frequency Drive :: Specifications
- ABB ACS800 AC Variable Frequency Drive :: Basic Type Code Information
- ABB ACS800 AC Variable Frequency Drive :: 230V Ratings (pricing)
- ABB ACS800 AC Variable Frequency Drive :: 380V Ratings (pricing)
- ABB ACS800 AC Variable Frequency Drive :: 460V Ratings (pricing)
- ABB ACS800 AC Variable Frequency Drive :: ACS 800-U2 NEMA 1 R7 & R8 Frame Size and ACS 800-02+C111 IP21 (NEMA 1) R7 & R8 Frame Size
- ABB ACS800 AC Variable Frequency Drive :: ACS 800 NEMA 1/12 R2 through R6 Frame Size
- ABB ACS800 AC Variable Frequency Drive :: ACS 800-02 NEMA 1 R7 & R8 Frame Size
- ABB ACS800 AC Variable Frequency Drive :: ACS 800-U4 Module R7 Frame Size
- ABB ACS800 AC Variable Frequency Drive :: ACS 800-U4 Module R8 Frame Size
- ABB ACS880 Industrial Low Voltage AC Drives
- ABB ACS880 AC Drives – Technical Data
- Wall-mounted single drives, ACS880-01
- ABB ACS880 Ratings, types and voltages
- ABB ACS880 AC Drives – Dimensions & Connectivity
- ABB ACS880 AC Drives – Standard Software
- ABB ACS880 AC Drives – Intuitive Human-Machine Interface
- ABB ACS880 AC Drives – Integrated Safety
- ABB ACS880 AC Drives – Flexible Connectivity
- Input/output Modules, Speed Feedback Interfaces & Communication Modules
- ABB Softstarters, Type SSM, Medium Voltage, 2300-13,800V :: Description
- ABB Type SSM Softstarters – Medium Voltage, 2300-13,800V :: General Information
- ABB Type SSM Soft Starters – Medium Voltage, 2300 – 13,800V :: Catalog Numbers
- ABB Soft Starters, Type SSM – Medium Voltage, 2300-13,800V :: Technical Data
- ABB Softstarters, Type SSM, Medium Voltage, 2300-13,800V :: Approx. Dimensions
- Yaskawa AC Drives
- AuCom Soft Starters
- Emerson Industrial Automation (Control Techniques and Saftronics) AC Drives
- Control Techniques – Commander SE AC Drive
- Control Techniques – Commander SK AC Drive
- Commander SK :: Features
- Commander SK :: Terminal Diagram and Description
- Commander SK :: Specifications and Dimensions
- Commander SK – Options :: Overview
- Commander SK – Options :: Configuration and Programming
- Commander SK :: Operator Interface
- Commander SK :: Power Accessories
- Commander SK :: Environmental Protection and Cable Management
- Commander SK :: Input / Output
- Commander SK :: Communication
- Commander SK :: Programming Software
- Control Techniques – Commander SX AC Drive
- Commander SX :: Features, Ratings, Prices and Ordering
- Commander SX :: Terminal Diagram and Description
- Commander SX:: Specifications and Dimensions
- Commander SX :: Options – Overview / Drive Configuration and Programming
- Commander SX :: Communication / Operator Interface
- Commander SX :: Power Accessories
- Commander SX :: Input/Output and Communication
- Control Techniques – Unidrive SP AC Drive
- Unidrive SP :: Features
- Unidrive SP :: Ratings, Prices & Ordering – Wall Mount
- Unidrive SP :: Ratings, Prices & Ordering – Free Standing Cubicle
- Unidrive SP :: Unidrive SP Regen Mode
- Unidrive SP :: Terminal Diagram and Description
- Unidrive SP :: Specifications and Dimensions
- Unidrive SP :: Options – Overview
- Unidrive SP :: Operator Interface
- Unidrive SP :: Power Accessories
- Unidrive SP :: Option & Feedback Modules
- Unidrive SP :: Option Input / Output Modules
- Unidrive SP :: Option Application / Programming Modules
- Unidrive SP :: Option Communication Modules
- Unidrive SP :: Drive Configuration and Programming
- Unidrive SP :: Application Programming Software
- Unidrive SP :: Pre-packaged Solutions
- Saftronics GP10 AC Drives
- Saftronics GP10 – Pricing, Dimensions & Weights
- Saftronics GP10 – Optional DC Link Reactors
- Saftronics GP10 – Options & Accessories
- Saftronics GP10 – Palm Pilot Saflink Kit
- Saftronics GP10 – SR10 Radio Modem Kit
- Saftronics GP10 – Relay Output Card
- Saftronics GP10 – Digital I/O Interface Card
- Saftronics GP10 – Analog I/O Interface Card
- Saftronics GP10 – SF-10 Ethernet Module
- Saftronics GP10 – Interface Option Card
- Saftronics GP10 – Under Torque Detection Option
- Saftronics GP10 – 24 VDC or 24/120 VAC Interface
- Saftronics GP10 – Air Pressure Sensor + V/I Converter Output Card
- Saftronics GP10 – HMI Pump Controller
- Saftronics GP10 – SDBU – Dynamic Brake Module
- Saftronics GP10 – 208-230V Dynamic Brake Packages
- Saftronics GP10 – 460V Dynamic Brake Packages
- Saftronics GP10 – Ratings Efficiency & Watts Loss
- Saftronics GP10 – Standard Specifications
- Saftronics GP10 – Basic Connection Diagram
- Saftronics GP10 – Basic Connection Diagram to PLC
- Saftronics GP10 – Basic Connection Diagram (Europe)
- Saftronics GP10 – Basic Connection to PLC (Europe)
- Saftronics S10 AC Drives
- Saftronics S10 – Options and Accessories
- Saftronics S10 – Standard Specifications
- Saftronics S10 – Dimensions
- Saftronics S10 – Dimensions – Part Number: S102002 – S102003 & S104001 – S104003
- Saftronics S10 – Dimensions – Part Number: S102F25 – S102001
- Saftronics S10 – Dimensions — Part Number: S102F25 – S102001 no Operators
- Saftronics S10 – Dimensions – Part Number: S102002-2003 & S104001-4003
- Saftronics S10 – Basic Wiring Diagram
- Saftronics CV10 AC Drives
- Saftronics CV10 – Part Numbers, Dimensions & Weights
- Saftronics CV10 – LED Keypad with Speed Pot
- Saftronics CV10 – LCD Keypad (supports 5 Languages)
- Saftronics CV10 – Keypad Extension Cable
- Saftronics CV10 – Communication Option Cards
- Saftronics CV10 – Bi-Polar Speed Reference Option Card
- Saftronics CV10 – Standard Specifications
- Saftronics CV10 – Ratings Efficiency and Watts Loss
- Saftronics CV10 – Dimensions Frame 1 – IP20 (Open Chassis)
- Saftronics CV10 – Dimensions Frame 1 – NEMA 1
- Saftronics CV10 – Dimensions Frame 2 – IP20 (Open Chassis)
- Saftronics CV10 – Dimensions Frame 2 – NEMA 1
- Saftronics CV10 – Dimensions Frame 3 – IP20 (Open Chassis)
- Saftronics CV10 – Dimensions Frame 3 – NEMA 1
- Saftronics CV10 – Basic Wiring Diagram
- Saftronics VG10 AC Drive
- Saftronics VG10 – Pricing, Dimensions & Weights
- Saftronics VG10 – Optional DC Link Reactors
- Saftronics VG10 – Options and Accessories
- Saftronics VG10 – Palm Pilot Saflink Kit
- Saftronics VG10 – Relay Output Card
- Saftronics VG10 – SR10 Radio Modem Kit
- Saftronics VG10 – Digital I/O Interface Card
- Saftronics VG10 – Analog I/O Interface Card
- Saftronics VG10 – SF-10 Ethernet Module
- Saftronics VG10 – PGX Encoder Feedback Card
- Saftronics VG10 – Encoder + Analog Output Card
- Saftronics VG10 – PG Feedback Card SOPCG11SPG
- Saftronics VG10 – PG Feedback Card SOPCG11SPG2
- Saftronics VG10 – Synchronized Operation Card
- Saftronics VG10 – 24 VDC or 24/120 VAC Interface Card Kit
- Saftronics VG10 – Air Pressure Sensor + V/I Converter Output Card
- Saftronics VG10 – SDBU – Dynamic Brake Module
- Saftronics VG10 – 208-230V Dynamic Brake Packages
- Saftronics VG10 – 460V Dynamic Brake Packages
- Saftronics VG10 – Ratings Efficiency and Watts Loss
- Saftronics VG10 – Standard Specifications
- Saftronics VG10 – DC Link Reactor 100 HP and Above
- Saftronics VG10 – Basic Connection Diagram (Sink Logic, Mainly America)
- Saftronics VG10 – Basic Connection Diagram to PLC (Sink Logic, Mainly America)
- Saftronics VG10 – Basic Connection Diagram (Source Logic, Mainly Europe)
- Saftronics VG10 – Basic Connection Diagram to PLC (Source Logic, Mainly Europe)
- Saftronics PC10 (Obsolete) AC Drives
- Saftronics PC10 – Options & Accessories
- Saftronics PC10 – SF-10 Ethernet Module Kit
- Saftronics PC10 – 24 VDC or 24/120 VAC Input + Relay Option Card
- Saftronics PC10 – 24 VDC or 24/120 VAC Interface Card Kit (PC10, GP10, or VG10 Inverter)
- Saftronics PC10 – Relay Output Card
- Saftronics PC10 – HMI Pump Controller
- Saftronics PC10 – PC10 120 VAC Option Card
- Saftronics PC10 – Palm Pilot Saflink Kit
- Saftronics PC10 – Dynamic Braking
- Saftronics PC10 – Drive Ratings Efficiency and Watts Loss
- Saftronics PC10 – Standard Specifications
- Saftronics PC10 – Part Number: PC102F12-9, PC102F25-9, PC102F50-9 & PC102001-9
- Saftronics PC10 – Part Number: PC102002-9, PC102003-9, PC104F50-9, PC104001-9, PC104002-9 & PC104003-9
- Saftronics PC10 – Part Number: PC102005-9 & PC104005-9
- Saftronics PC10 – Part Number: PC102007-9, PC102010-9, PC104007-9 & PC104010-9
- Saftronics PC10 – NEMA 1 Kit Dimensions
- Saftronics PC10 – Basic Wiring Diagram
- Fincor 5700 Series (Obsolete) AC Drive
- Fincor 5740 Series (Obsolete) AC Drive
- Fincor 5750 Series (Obsolete) AC Drives
- Motortronics Soft Starters
- SOLCON Soft Starters
- SOLCON RVS-DN Digital Soft Starter with Advanced Motor Protection
- Solcon HRVS-DN Digital Soft Starter with Advanced Motor Protection
- Solcon HRVS-TX Digital Transformer Soft Starter
- SOLCON RVS-AX Analog Soft Starters
- SOLCON Solstart Plus Analog Soft Starters
- SOLCON RVS-BX Basic Soft Starter with Built-In Bypass
- SOLCON RVS-DX Digital Soft Starter with Built-In Bypass
- SOLCON RVS-EX Digital Soft Starter for Explosion Proof motors with Built-In Bypass
- SOLCON SEM-N Rugged Soft Starter for Naval and Military Specifications
- SOLCON SOLSTART Miniature Analogue Soft Starter
- SOLCON SOLSTART 1P Single Phase Analogue Soft Starter
- SOLCON SOLBRAKE DC Injection Brake Soft Starter
- Magnetek – Soft Starters
- WEG Variable Frequency Drives, Controls and Motors
- ABB ACS150 Component Drives :: Overview
- DC Variable Speed Drives
- DC Drive Fundamentals
- ABB DCS 400 Digital DC Converter Drive
- ABB DCS 500 DC Drive
- ABB DCS800 DC Drives Overview
- DCS800 – Power Converter Modules
- DCS800 Panel Drive
- DCS800 Enclosed Converters
- DCS800 Rebuild and Upgrade Kits
- Adaptive Programming and Start-up Assistants
- DriveWindow Light – Startup and Maintenance Tool
- DCS800 Commissioning Macros
- DCS800 Firmware
- DCS800 Technical Specifications
- Current Ratings – Modules – Non-Regenerative
- Current Ratings – Modules – Regenerative
- Current Ratings – Modules – DCS800-EP Panel Drive
- DCS800 Dimensions and Weights
- DCS800 Technical Diagram
- DCS800 Plug-in Options
- DCS800 Feedback Options
- DCS800 Communication Options – Fieldbus Control
- DCS800 External Field Supply
- ABB DCS800-EP replaces Reliance FlexPak® 3000 – 230V Drive Cross Reference
- ABB DCS800-EP – 460V Drive Cross Reference
- ABB DCS800-EP – Options Cross Reference
- ABB DCS800-EP – Product Differences and Remedies – Hardware
- ABB DCS800-EP – Product Differences and Remedies – Control/Interface & Features
- ABB DCS800-EP – Drive Dimensions
- ABB DCS800-EP – Installation Procedure – Wiring and Configuration
- ABB DCS800-EP – Parameter Cross-Reference
- FINCOR Series 2600/2610 DC Drives
- 50 Amp & 90 Amp DC Field Regulators
- Mentor II | Quantum III | FXM5 Change of Status
- SIMOREG 6RA24 Siemens DC Drive Features
- SIMOREG 6RA70 Siemens Variable Speed DC Drive Description and Base Drive Catalog Numbers
- SIMOREG 6RA70 Siemens DC Drive Features
- SIMOREG 6RA70 DC Master Design & Operation – Converters
- SIMOREG 6RA70 Design & Operation – Parameterization Devices
- SIMOREG 6RA70 Design & Operation – Software Structure
- SIMOREG 6RA70 Design & Operation – Closed-Loop Functions in Armature Circuit
- SIMOREG 6RA70 Design & Operation – Closed-Loop in Field Circuit
- SIMOREG 6RA70 Design & Operation – Optimization Run
- SIMOREG 6RA70 Design & Operation – Monitoring & Disgnosis
- SIMOREG 6RA70 Design & Operation – Functions of Inputs & Outputs
- SIMOREG 6RA70 Design & Operation – Safety Shutdown (E-STOP)
- SIMOREG 6RA70 Design & Operation – Serial Interface
- 1000 Hp DC Variable Speed Drive System
- 3000 Hp DC Variable Speed Drive
- Permanent Magnet DC Motors
- SCR Drive Controllers (SCR-Silicon Controlled Rectifier)
- Custom Electric Control Panel Shop
- GE AC & DC Motors (G.E. Motors – General Electric AC & DC Motor)
- GE X$D Ultra® NEMA Premium Efficiency – TEFC AC Motors
- GE Kinamatic® Explosion Proof AC Motors
- GE Energy Saver® – TEFC Severe Duty AC Motors
- GE Kinamatic® General Purpose AC Motors
- GE Motors Energy Saver NEMA Premium Efficiency – ODP AC Motors
- GE ValueLine™ EPAct Efficiency – TEFC AC Motors
- GE ValueLine™ EPAct Efficiency – ODP AC Motors
- GE Permanent Magnet Custom DC Motors
- GE ValueLine™ Vertical Hollow Shaft AC Motors
- GE Permanent Magnet Standard DC Motors
- GE ASD Inverter Duty AC Motors
- G.E. Permanent Magnet Washdown DC Motors
- Avtron – Drives, Measurement and Tachs
- Avtron – Adjustable Speed Drives and Drive Systems
- Avtron – Speed and Length Measurement
- Avtron – Tachs, Tachometers, Encoders, Rotary Pulse Generators
- Avtron – Sales Literature and Instruction Sheets
- Avtron – Classic Tach Models
- Avtron – Price Quotation Request Form
- Avtron – Tachometers Availability
- Avtron – Heavy, Mill-Duty Encoders
- Avtron – Setting Air Gap on M285 Sensors
- Avtron – M4 Universal Encoder
- Avtron – M56, M67, M85 THIN-LINE
- Avtron – M285QUAD Outline Drawing
- Avtron – Severe Duty Encoders
- Avtron – Mill-Duty Encoders
- Avtron – M3 Universal Encoder
- Avtron – M3 Applications
- Avtron – M3 Installation
- Avtron – M3 Specifications
- Avtron – Tach Accessories
- Avtron – Tach Solutions
- Avtron – Rugged Environments
- Avtron – Selection by Motor Frame Size
- Avtron – Adapter Kits Outline Drawings
- Avtron – Motors with Brakes
- Avtron – NEMA C Face Mounting
- Avtron – Market Specific Applications
- Dynapar Encoders and Tachs
- ACURO AI25 Encoders
- Acuro Series AI25 Absolute Encoder with DeviceNet Interface
- Acuro Series AI25 Absolute Encoder with Profibus Interface
- Acuro Series AI25 Absolute Encoder with Interbus Interface
- Acuro Series AI25 Absolute Encoder with BiSS Interface
- Acuto Series AI25 Optical Encoders with SSI Interface
- Acuro Series AI25 Absolute Encoder with Parallel Interface
- Acuro Series AD25 Drive Absolute Encoder
- Series R25 – Mill Duty, HOUSED Resolver
- Series 21/22 Heavy Duty Incremetal Encoders
- Series H20 Encoder
- Series HA25 Dynapar Heavy Duty Encoders
- Series HR25 Incremental Encoders
- Series HC25 Incremental Encoders
- Series H58 Heavy Duty Encoders
- Series H42 Heavy Duty Encoders
- Series HA725 Indusrtial Duty Encoders
- Series HD20 Optical Encoder
- Series HD25 Optical Encoder – Harsh Duty
- Series H56 Rotopulser Heavy Duty Encoders
- RIM Tach 6200 Digital Tachometer
- Series X25 Incremental Encoders
- Series 60 Rotopulser Incremental Encoders
- Series H20 Hub Shaft Encoders
- Series HSD25 Harsh Duty Optical Encoders
- Series HSD44
- Series HS20 Sealed Hollow Shaft Encoders
- Series HS35 Sealed Hollow Shaft Encoders
- The NEW HS35R
- Series HSD35 Shaftless Optical Encoder
- Series HSD37 Hollowshaft Rotary Encoder
- Series HSD38 Harsh Duty Optical Encoder
- Series DWD38 Heavy Duty Rotary Encoders
- SLIM Tach HS56 Incremental Encoder / Tachometer
- RIM Tach HS85 Digital Tachometer
- SLIM Tach SL56 Rotary Encoder
- SLIM Tach RL67 Incremental Rotary Encoder
- SLIM Tach SL85 Digital Tachometer
- SLIM Tach SL1250 Incremental Encoder
- RIM Tach 8500 Digital Tachometer
- RIM Tach 1250 Digital Tachometer
- Series R45 Rotopulser Incremental Encoders
- ACURO AI25 Encoders
- Spare Parts and Replacement Parts
- PLC (Programmable Logic Controllers)
- Services
- Projects
- Operator Stations by Joliet Technologies
- AC VFD, AC Controllers and DC VSD by Joliet Technologies
- Material Handling Modernization Project by Joliet Technologies
- 10 DC (SCR) Drive System :: Neptune Marine Oil & Gas
- Mermaid Offshore Services :: 4 DC (SCR) Drive Cabinets
- “Frontier Driller” Offshore Oil Rig :: DC (SCR) Drive Bays
- 1000Hp Siemens SIMOREG 6RA70 DC Variable Speed Drive Retro-Fit
- Smurfit-Stone: Corrugator Crew Sets Production Record
- Steel Slitting Line for Braner USA
- 1000HP DC Drive, Bow Thruster Application for Pegler Automation
- 1000HP DC Traction Motor Drive, Slurry Pump Application for Baker Hughes
- Siemens 6RA70 DC Drive and GE 752 Traction Motor to Hallett Materials
- ABB ACS 800 VFD to Applied Synergistic
- Two 200Hp Variable Speed DC Drives and Motors to JHT Electronics
- Substrate Technology Inc. :: Joliet Technologies, L.L.C.
- Wyco Tool Company
- Variable Frequency Drives and Controls for Food Processing and Bakery Machinery
- Information
- Guide to Harmonics with AC Variable Frequency Drives
- Variable Speed Drives – Application Information
- Reducing harmonics caused by variable speed drives
- FAQ – Variable Speed Drives Frequently Asked Questions
- EASA Electrical Engineering Handbook
- Part Winding Start
- 3Ph Motors, Single Speed
- 3Ph Motors, 2 Speed, Single Winding
- Connections for NEMA DC Motors
- Connections for NEMA DC Generators
- Field Polarities of DC Machines
- Maximum Locked-Rotor Currents – Three-Phase Squirrel Cage Motors
- NEMA Code Letters for AC Motors
- General Speed-Torque Characteristics
- Effect of Voltage unbalance on Motor Performance
- Starting Characteristics of Squirrel Cage Induction Motors
- Allowable Starts and Starting Intervals
- NEMA Size Starters for Three-Phase Motors
- Starter Enclosures
- NEMA Size Starters for Single-Phase Motors
- Determining the Polarization Index of Machine Windings
- Formulas for Electrical Motors
- Motor Application Formulas
- Glossary of Terms
- Variable Frequency Drive (VFD) Case Studies
- VFD Case Studies – ABB drives & motors help to launch lifeboats quickly and safely.
- VFD Case Studies – Paperboard mill benefits from using DC drives
- VFD Case Studies – ABB Drive cuts water pumping bill for semiconductor plant.
- VFD Case Studies – Insulation manufacturing process saves energy with ABB :: Joliet Technologies
- VFD Case Studies – ABB drives cut costs at MINI production plant
- VFD Case Studies – Film maker slashes costs with ABB drives
- VFD Case Studies – ABB drive cuts costs for wooden toy company
- VFD Case Studies – Close pump control doubles efficiency for West of Scotland Water
- VFD Case Studies – ABB Energy Appraisal Saves Money :: Joliet Technologies
- VFD Case Studies – Staggering energy savings prove value of professional audit
- VFD Case Studies – Soft starters save costs for mechanical engineers
- NEMA Frame Chart and T-Frame Chart :: Joliet Technologies
- Model 1681 Instruction Manual – Firing Circuits DC SCR Drives
- IGBT – Insulated Gate Bipolar Transistors :: Joliet Technologies
- Blog
Blog
2026 Top Variable Frequency Drive Types?
Choosing the right variable frequency drive in 2026 requires more than comparing power ratings and prices. Modern facilities expect quieter motors, lower energy use, reliable communication, and precise speed control. Yet many buyers still focus only on horsepower. That approach can create avoidable problems.
This guide examines the top variable frequency drive types shaping industrial applications in 2026. It covers voltage source inverter drives, current source inverter drives, regenerative drives, sensorless vector drives, and closed-loop vector systems. Each type responds differently to starting torque, braking demands, motor feedback, and load changes. A conveyor carrying uneven boxes needs different control than a pump moving water through long pipes.
Real-world performance depends on installation details. Cable length, motor insulation, ambient temperature, harmonics, and enclosure protection can change the final result. A technically advanced drive may underperform when ventilation is poor or parameters are copied incorrectly. Small details matter.
The discussion also compares drive suitability across manufacturing lines, HVAC systems, elevators, compressors, and renewable energy equipment. It uses practical selection principles supported by established engineering practice and manufacturer documentation. Readers will see where each type performs well, where it becomes expensive, and where its limits deserve attention.
No single drive wins every application. That is worth remembering. Technology changes quickly, but sound sizing remains essential. The best choice balances efficiency, control accuracy, maintenance skill, motor compatibility, and total operating cost. This 2026 overview aims to make that decision clearer, while acknowledging that real equipment rarely behaves exactly like a catalogue example.
What Is a Variable Frequency Drive and How Does It Work?
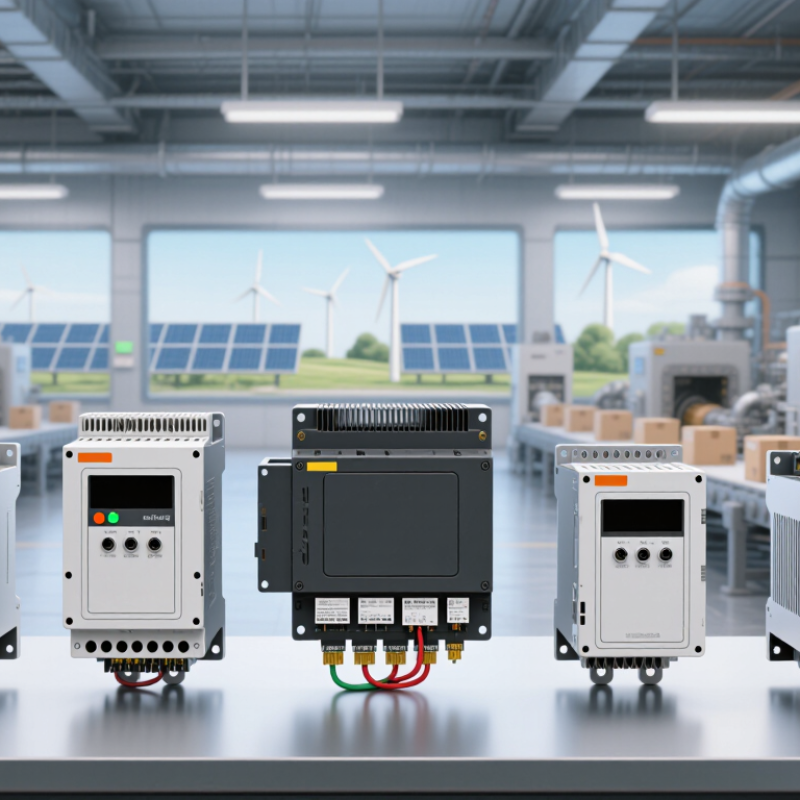
A variable frequency drive, or VFD, controls an AC motor by changing its electrical frequency and voltage. Lower frequency usually means slower motor speed. Higher frequency allows faster operation within safe limits. The drive first converts incoming AC power into DC through a rectifier. A DC bus smooths that energy with capacitors and filtering components. Then, an inverter rapidly switches the DC supply into a controlled AC waveform. This process uses pulse-width modulation, often called PWM.
The best VFD type depends on the machine, motor, and control accuracy required in 2026. Basic volts-per-hertz drives suit fans, pumps, and conveyors with steady loads. Sensorless vector drives provide stronger starting torque without a motor encoder. Closed-loop vector drives use feedback for precise speed and position control. Regenerative drives can return braking energy to the electrical system, but they require careful system design. Medium-voltage drives serve larger industrial motors and demand stricter installation practices.
In a real panel, heat matters. Dust matters too. A drive may show perfect settings but still fail in a poorly ventilated enclosure. Correct motor data, cable grounding, overload protection, and acceleration settings improve reliability. I would not choose a drive from horsepower alone. That shortcut often misses starting torque and braking needs. No drive is perfect. Even advanced control can perform poorly when the motor condition, wiring, or load changes unexpectedly. Testing under actual operating conditions remains essential.
How Are Variable Frequency Drives Classified by Control Method?
2026 Top Variable Frequency Drive Types?
How Are Variable Frequency Drives Classified by Control Method?
Variable frequency drives are commonly classified by how they control motor voltage, frequency, and torque. The simplest method is scalar control, often called volts-per-hertz control. It maintains a planned voltage-to-frequency ratio. This approach suits fans, pumps, and conveyors with steady load patterns. It is cost-effective, but speed accuracy can weaken under sudden load changes.
Sensorless vector control estimates motor position and torque without an encoder. It responds faster than scalar control and performs better during acceleration. Technicians often use it for mixers, compressors, and material-handling equipment. However, motor data must be entered accurately. A poor setup can cause unstable speed or unnecessary current.
Closed-loop vector control uses an encoder to measure shaft speed continuously. It provides stronger torque at low speed and more precise positioning. This method fits hoists, winders, and demanding production machines. Some drives also use direct torque control, which adjusts motor torque rapidly through real-time calculations. Its response can be excellent, though tuning and maintenance may require deeper expertise.
In practical commissioning, the control label alone is not enough. Motor condition, cable length, load inertia, and operating temperature also affect results. The boundaries between control categories are not perfectly clean. A drive advertised as “vector” may perform differently across applications. Engineers should test acceleration, braking, and low-speed stability before approving the final setting. Small details matter.
What Are the Main Types of Variable Frequency Drives in 2026?
What Are the Main Types of Variable Frequency Drives in 2026?
Variable frequency drives mainly fall into AC drives, DC drives, and servo drives. AC drives control induction and permanent-magnet motors by adjusting frequency and voltage. They dominate general industrial applications, including pumps, fans, conveyors, and compressors. Fortune Business Insights valued the global VFD market at about USD 25.84 billion in 2024, showing strong demand for efficient motor control.
DC drives still serve older production lines because they provide strong starting torque and simple speed control. However, maintenance requirements and brush wear limit new installations. Servo drives offer precise position, speed, and torque control. They suit robotics, packaging equipment, and high-speed motion systems. They cost more, but accuracy can justify the investment.
Engineers also classify AC drives by inverter design. Voltage-source inverters remain common, while current-source inverters support certain high-power applications. Matrix converters provide compact conversion, but their control complexity can challenge maintenance teams. According to the International Energy Agency, electric motor systems consume roughly half of global electricity. The right drive therefore affects more than speed. It influences heat, downtime, power quality, and operating cost. The classification is not perfectly clean. Some modern drives combine features from several categories, so application conditions matter more than a simple product label. Industry references include the International Energy Agency’s Energy Efficiency 2023 report and IEC 61800-2.
How Do VFD Types Differ in Performance, Cost, and Application?
2026 Top Variable Frequency Drive Types: Performance, Cost, and Application
Variable frequency drives differ mainly in control accuracy, response speed, and installation cost. Basic V/f drives are usually the lowest-cost option. They suit pumps, fans, and conveyors with steady loads. Their control feels predictable, but torque weakens at low speed.
Sensorless vector drives improve low-speed torque without requiring an encoder. They fit compressors, mixers, and material-handling equipment. Closed-loop vector drives use encoder feedback for precise speed and torque control. They perform better on cranes, extruders, and machines requiring rapid load changes.
Medium-voltage drives serve large motors and high-power processes. Their hardware and commissioning costs are substantially higher.
The U.S. Department of Energy reports that motor systems consume about 69% of industrial electricity in American manufacturing. This makes drive selection more important than the purchase price alone. A correctly sized drive can reduce throttling losses in variable-torque applications. However, savings depend on load profile, operating hours, and maintenance quality.
Market research reports also identify energy efficiency and industrial automation as major VFD growth drivers through the decade. Still, not every premium drive delivers a sensible return. A low-cost V/f drive may outperform an advanced model when the application is simple.
I have seen specifications become unnecessarily complex. Harmonics, heat, cable length, and motor compatibility also require checking. Ignoring these details can erase expected savings. Performance is valuable, but only when the process truly needs it.
How Can You Choose the Right Variable Frequency Drive Type?
2026 Top Variable Frequency Drive Types?
How Can You Choose the Right Variable Frequency Drive Type?
Choosing a variable frequency drive starts with the machine, not the catalog. A fan or centrifugal pump often works well with simple V/f control. This option is economical and easy to commission. A conveyor, mixer, or compressor may need sensorless vector control for stronger starting torque. Check the motor’s rated current, overload demand, speed range, and acceleration time.
Low-speed lifting equipment usually needs closed-loop vector control with feedback. The encoder helps maintain torque when speed falls near zero. Regenerative drives suit elevators, downhill conveyors, and test rigs that return energy during braking. Large industrial motors may require medium-voltage drives, but installation conditions become more demanding. Cable length, cooling, enclosure rating, and harmonic limits matter.
Field experience shows that a drive sized only by motor horsepower can disappoint. I have seen applications fail because the load torque was ignored. Paperwork looked correct. The machine still stalled. Consider dust, heat, washdown water, and frequent starts before choosing the enclosure. Confirm whether the motor supports inverter operation and whether braking resistors are necessary. A technical review with the motor supplier and a qualified controls engineer reduces avoidable errors. It may cost more initially. That is not always wasteful.
| VFD Type | Control Method | Typical Speed Accuracy | Typical Torque Capability | Energy Efficiency | Regenerative Operation | Main Advantages | Typical Applications | Key Selection Considerations |
|---|---|---|---|---|---|---|---|---|
| Scalar V/Hz Drive | Maintains a relatively constant voltage-to-frequency ratio. Slip compensation may be included. | Approximately ±1% to ±3% of base speed, depending on motor and load conditions. | Suitable for standard starting and running torque requirements; limited low-speed torque control. | Good for fixed-speed reduction Efficiency depends strongly on motor loading and system design. |
Usually not available without additional braking hardware. | Simple setup, low cost, broad motor compatibility, and easy commissioning. | Fans, pumps, blowers, conveyors, and other variable-torque loads. | Choose when precise speed regulation and high starting torque are not critical. Confirm motor compatibility and required acceleration torque. |
| Sensorless Vector Drive | Estimates motor flux and rotor position from electrical measurements without an encoder. | Typically about ±0.5% to ±1% of base speed after motor tuning. | Provides stronger starting and low-speed torque than basic V/Hz control; often suitable for roughly 100% to 150% overload for limited periods, depending on the drive rating. | Very good Improves motor control across changing loads without an external speed sensor. |
Dynamic braking is commonly supported; true regeneration requires a suitable regenerative system. | Good balance of performance, cost, installation simplicity, and control capability. | Conveyors, mixers, compressors, machine tools, hoists with moderate performance requirements, and material-handling equipment. | Choose when load changes, low-speed torque, and speed regulation matter but an encoder is undesirable or impractical. |
| Closed-Loop Vector Drive | Uses an encoder or resolver feedback signal to regulate motor speed, torque, and position. | Commonly about ±0.01% to ±0.1% of rated speed, depending on feedback resolution and tuning. | High starting torque and precise torque control; suitable for demanding overload and low-speed applications when correctly sized. | Excellent under varying loads Maintains motor control efficiently over a wide speed range. |
Regeneration may be integrated when paired with the correct braking or regenerative front-end equipment. | High speed accuracy, strong low-speed performance, precise torque control, and improved load response. | Cranes, elevators, winders, extruders, printing lines, tension-control systems, and precision conveyors. | Choose when speed regulation, torque response, positioning, or load sharing is more important than minimum installation cost. |
| Direct Torque Control Drive | Controls motor torque and flux directly using rapid switching decisions and motor-model calculations. | High dynamic speed response; final accuracy depends on feedback configuration, motor model, and application setup. | Very fast torque response and strong performance during rapid load changes. | Excellent dynamic efficiency Can reduce motor losses in demanding variable-load operation when properly tuned. |
Possible with an appropriate regenerative converter or braking arrangement. | Fast torque response, reduced dependence on conventional modulation loops, and strong dynamic performance. | High-performance winding, test stands, large rotating equipment, high-dynamic machinery, and demanding process lines. | Choose when rapid torque response and dynamic control justify a more advanced commissioning process and higher system complexity. |
| Regenerative VFD System | Uses an active front end or regenerative converter to return braking energy to the electrical grid. | Depends on the selected motor-control method; commonly paired with vector or closed-loop vector control. | Suitable for frequent braking, four-quadrant operation, and loads that repeatedly accelerate and decelerate. | Best for energy recovery Reduces energy dissipation compared with resistor braking in suitable duty cycles. |
Yes; designed for controlled power flow from the motor back to the supply. | Energy recovery, reduced braking-resistor heat, continuous braking capability, and four-quadrant operation. | Elevators, cranes, centrifuges, test benches, downhill conveyors, and high-inertia machinery. | Choose when braking energy is frequent or substantial. Evaluate regeneration power, harmonic performance, grid requirements, and cooling needs. |
| Medium-Voltage VFD | Uses a medium-voltage power-conversion architecture with a motor-control strategy such as V/Hz or vector control. | Depends on the control method, motor, feedback, and operating point. | Designed for high-power motors and large industrial loads; overload capability varies by duty classification. | High system-level potential Can substantially reduce throttling and mechanical losses in large variable-torque systems. |
Available in selected configurations; braking and regeneration require application-specific engineering. | Suitable for high-power motors, reduced mechanical stress during starting, and efficient process-speed control. | Large pumps, fans, compressors, mills, conveyors, and process equipment in heavy industry. | Choose based on motor voltage, power rating, short-circuit requirements, harmonic limits, bypass needs, cooling, service access, and operator safety. |
| Multi-Motor VFD | One drive controls multiple motors, generally with matched motors operating at the same commanded frequency. | Typically adequate for synchronized speed control; individual motor speed accuracy is limited without separate feedback and drives. | Combined motor current must remain within the drive rating; individual overload behavior must be evaluated carefully. | Efficient for coordinated loads Can reduce equipment count when independent motor control is unnecessary. |
Usually limited unless the system is specifically engineered for shared regenerative operation. | Lower panel count, coordinated operation, and simplified speed reference architecture. | Parallel fans, grouped pumps, simple conveyor sections, and mechanically synchronized machines. | Choose only when motors have compatible characteristics and independent speed, torque, protection, and feedback control are not required. |
| Single-Phase Input VFD | Converts single-phase input power to a variable-frequency output, commonly for compatible three-phase motors at smaller ratings. | Depends on the implemented V/Hz or vector-control algorithm and motor setup. | Output current and overload capacity are often restricted by the single-phase input and thermal design. | Good for small equipment Can provide variable-speed control where three-phase utility power is unavailable. |
Usually limited; confirm braking and regeneration specifications before selection. | Allows variable-speed control in facilities with single-phase supply and can reduce the need for mechanical speed control. | Small pumps, fans, machine tools, workshop equipment, and light-duty conveyors. | Check input current, derating requirements, motor connection, output phase configuration, starting load, and available short-circuit capacity. |
Related Posts
-
Top 10 Types of Variable Frequency Drives
-
What Is a VFD Variable Frequency Drive and How Does It Work?
-
What Is a Frequency Drive and How Does It Work?
-
Top 10 AC Motor Speed Controllers to Enhance Your Efficiency in 2023
-
How to Optimize Energy Efficiency with Variable Frequency Drives: Key Insights and Data
-
How to Choose the Right Variable Speed DC Motor for Your Needs?