- Home
- Request for Quote
- Products
- Variable Frequency Drive Systems and Controls
- AC Variable Frequency Drives
- ABB ACS150 Component Drives :: Overview
- ABB ACS150 Component Drives :: Technical Specifications
- ABB ACS150 Component Drives :: Ratings, Types, Voltages and Construction – Prices
- ABB ACS150 Component Drives :: Dimensions, Weight and Noise
- ABB ACS150 Component Drives :: Interface and Options (prices)
- ABB ACS150 Component Drives :: Technical Data
- ABB ACS150 Component Drives :: Control Connections
- ABB ACS350 General Machinery Drives :: Overview
- ABB ACS350 General Machinery Drives :: Technical Specifications
- ABB ACS350 General Machinery Drives :: Ratings, Types, Voltages and Construction
- ABB ACS350 General Machinery Drives :: Dimensions, Weight and Noise
- ABB ACS350 General Machinery Drives :: Interface and Options (prices)
- ABB ACS350 General Machinery Drives :: Technical Data
- ABB ACS350 General Machinery Drives :: Control Connections
- ABB ACS550 AC Variable Frequency Drive :: Overview
- ABB ACS550 AC Variable Frequency Drive :: Hardware Description
- ABB ACS550 AC Variable Frequency Drive :: Standard Features and Options
- ABB ACS550 AC Variable Frequency Drive :: Specifications
- ABB ACS550 AC Variable Frequency Drive :: 230V Ratings (pricing)
- ABB ACS550 AC Variable Frequency Drive :: 380V Ratings (pricing)
- ABB ACS550 AC Variable Frequency Drive :: 480V Ratings (pricing)
- ABB ACS550 AC Variable Frequency Drive :: Dimensions: ACS550 NEMA 1 R1 through R6 Frame Size
- ABB ACS550 AC Variable Frequency Drive :: Dimensions: ACS550 NEMA 12 R1 through R6 Frame Size
- ABB ACS550 AC Variable Frequency Drive :: Dimensions: ACS550-02 NEMA 1 R7 Frame Size
- ABB ACS550 AC Variable Frequency Drive :: Dimensions: ACS550-02 NEMA 1 R8 Frame Size
- ABB ACS550 AC Variable Frequency Drive :: Dimensions: ACS550-U2 NEMA 1 R7 & R8 Frame Size
- ABB ACS 600 Adjustable Speed AC Drives
- ABB ACS800 AC Variable Frequency Drive :: Overview
- ABB ACS800 AC Variable Frequency Drive :: Standard Features / Available Options and Software
- ABB ACS800 AC Variable Frequency Drive :: Specifications
- ABB ACS800 AC Variable Frequency Drive :: Basic Type Code Information
- ABB ACS800 AC Variable Frequency Drive :: 230V Ratings (pricing)
- ABB ACS800 AC Variable Frequency Drive :: 380V Ratings (pricing)
- ABB ACS800 AC Variable Frequency Drive :: 460V Ratings (pricing)
- ABB ACS800 AC Variable Frequency Drive :: ACS 800-U2 NEMA 1 R7 & R8 Frame Size and ACS 800-02+C111 IP21 (NEMA 1) R7 & R8 Frame Size
- ABB ACS800 AC Variable Frequency Drive :: ACS 800 NEMA 1/12 R2 through R6 Frame Size
- ABB ACS800 AC Variable Frequency Drive :: ACS 800-02 NEMA 1 R7 & R8 Frame Size
- ABB ACS800 AC Variable Frequency Drive :: ACS 800-U4 Module R7 Frame Size
- ABB ACS800 AC Variable Frequency Drive :: ACS 800-U4 Module R8 Frame Size
- ABB ACS880 Industrial Low Voltage AC Drives
- ABB ACS880 AC Drives – Technical Data
- Wall-mounted single drives, ACS880-01
- ABB ACS880 Ratings, types and voltages
- ABB ACS880 AC Drives – Dimensions & Connectivity
- ABB ACS880 AC Drives – Standard Software
- ABB ACS880 AC Drives – Intuitive Human-Machine Interface
- ABB ACS880 AC Drives – Integrated Safety
- ABB ACS880 AC Drives – Flexible Connectivity
- Input/output Modules, Speed Feedback Interfaces & Communication Modules
- ABB Softstarters, Type SSM, Medium Voltage, 2300-13,800V :: Description
- ABB Type SSM Softstarters – Medium Voltage, 2300-13,800V :: General Information
- ABB Type SSM Soft Starters – Medium Voltage, 2300 – 13,800V :: Catalog Numbers
- ABB Soft Starters, Type SSM – Medium Voltage, 2300-13,800V :: Technical Data
- ABB Softstarters, Type SSM, Medium Voltage, 2300-13,800V :: Approx. Dimensions
- Yaskawa AC Drives
- AuCom Soft Starters
- Emerson Industrial Automation (Control Techniques and Saftronics) AC Drives
- Control Techniques – Commander SE AC Drive
- Control Techniques – Commander SK AC Drive
- Commander SK :: Features
- Commander SK :: Terminal Diagram and Description
- Commander SK :: Specifications and Dimensions
- Commander SK – Options :: Overview
- Commander SK – Options :: Configuration and Programming
- Commander SK :: Operator Interface
- Commander SK :: Power Accessories
- Commander SK :: Environmental Protection and Cable Management
- Commander SK :: Input / Output
- Commander SK :: Communication
- Commander SK :: Programming Software
- Control Techniques – Commander SX AC Drive
- Commander SX :: Features, Ratings, Prices and Ordering
- Commander SX :: Terminal Diagram and Description
- Commander SX:: Specifications and Dimensions
- Commander SX :: Options – Overview / Drive Configuration and Programming
- Commander SX :: Communication / Operator Interface
- Commander SX :: Power Accessories
- Commander SX :: Input/Output and Communication
- Control Techniques – Unidrive SP AC Drive
- Unidrive SP :: Features
- Unidrive SP :: Ratings, Prices & Ordering – Wall Mount
- Unidrive SP :: Ratings, Prices & Ordering – Free Standing Cubicle
- Unidrive SP :: Unidrive SP Regen Mode
- Unidrive SP :: Terminal Diagram and Description
- Unidrive SP :: Specifications and Dimensions
- Unidrive SP :: Options – Overview
- Unidrive SP :: Operator Interface
- Unidrive SP :: Power Accessories
- Unidrive SP :: Option & Feedback Modules
- Unidrive SP :: Option Input / Output Modules
- Unidrive SP :: Option Application / Programming Modules
- Unidrive SP :: Option Communication Modules
- Unidrive SP :: Drive Configuration and Programming
- Unidrive SP :: Application Programming Software
- Unidrive SP :: Pre-packaged Solutions
- Saftronics GP10 AC Drives
- Saftronics GP10 – Pricing, Dimensions & Weights
- Saftronics GP10 – Optional DC Link Reactors
- Saftronics GP10 – Options & Accessories
- Saftronics GP10 – Palm Pilot Saflink Kit
- Saftronics GP10 – SR10 Radio Modem Kit
- Saftronics GP10 – Relay Output Card
- Saftronics GP10 – Digital I/O Interface Card
- Saftronics GP10 – Analog I/O Interface Card
- Saftronics GP10 – SF-10 Ethernet Module
- Saftronics GP10 – Interface Option Card
- Saftronics GP10 – Under Torque Detection Option
- Saftronics GP10 – 24 VDC or 24/120 VAC Interface
- Saftronics GP10 – Air Pressure Sensor + V/I Converter Output Card
- Saftronics GP10 – HMI Pump Controller
- Saftronics GP10 – SDBU – Dynamic Brake Module
- Saftronics GP10 – 208-230V Dynamic Brake Packages
- Saftronics GP10 – 460V Dynamic Brake Packages
- Saftronics GP10 – Ratings Efficiency & Watts Loss
- Saftronics GP10 – Standard Specifications
- Saftronics GP10 – Basic Connection Diagram
- Saftronics GP10 – Basic Connection Diagram to PLC
- Saftronics GP10 – Basic Connection Diagram (Europe)
- Saftronics GP10 – Basic Connection to PLC (Europe)
- Saftronics S10 AC Drives
- Saftronics S10 – Options and Accessories
- Saftronics S10 – Standard Specifications
- Saftronics S10 – Dimensions
- Saftronics S10 – Dimensions – Part Number: S102002 – S102003 & S104001 – S104003
- Saftronics S10 – Dimensions – Part Number: S102F25 – S102001
- Saftronics S10 – Dimensions — Part Number: S102F25 – S102001 no Operators
- Saftronics S10 – Dimensions – Part Number: S102002-2003 & S104001-4003
- Saftronics S10 – Basic Wiring Diagram
- Saftronics CV10 AC Drives
- Saftronics CV10 – Part Numbers, Dimensions & Weights
- Saftronics CV10 – LED Keypad with Speed Pot
- Saftronics CV10 – LCD Keypad (supports 5 Languages)
- Saftronics CV10 – Keypad Extension Cable
- Saftronics CV10 – Communication Option Cards
- Saftronics CV10 – Bi-Polar Speed Reference Option Card
- Saftronics CV10 – Standard Specifications
- Saftronics CV10 – Ratings Efficiency and Watts Loss
- Saftronics CV10 – Dimensions Frame 1 – IP20 (Open Chassis)
- Saftronics CV10 – Dimensions Frame 1 – NEMA 1
- Saftronics CV10 – Dimensions Frame 2 – IP20 (Open Chassis)
- Saftronics CV10 – Dimensions Frame 2 – NEMA 1
- Saftronics CV10 – Dimensions Frame 3 – IP20 (Open Chassis)
- Saftronics CV10 – Dimensions Frame 3 – NEMA 1
- Saftronics CV10 – Basic Wiring Diagram
- Saftronics VG10 AC Drive
- Saftronics VG10 – Pricing, Dimensions & Weights
- Saftronics VG10 – Optional DC Link Reactors
- Saftronics VG10 – Options and Accessories
- Saftronics VG10 – Palm Pilot Saflink Kit
- Saftronics VG10 – Relay Output Card
- Saftronics VG10 – SR10 Radio Modem Kit
- Saftronics VG10 – Digital I/O Interface Card
- Saftronics VG10 – Analog I/O Interface Card
- Saftronics VG10 – SF-10 Ethernet Module
- Saftronics VG10 – PGX Encoder Feedback Card
- Saftronics VG10 – Encoder + Analog Output Card
- Saftronics VG10 – PG Feedback Card SOPCG11SPG
- Saftronics VG10 – PG Feedback Card SOPCG11SPG2
- Saftronics VG10 – Synchronized Operation Card
- Saftronics VG10 – 24 VDC or 24/120 VAC Interface Card Kit
- Saftronics VG10 – Air Pressure Sensor + V/I Converter Output Card
- Saftronics VG10 – SDBU – Dynamic Brake Module
- Saftronics VG10 – 208-230V Dynamic Brake Packages
- Saftronics VG10 – 460V Dynamic Brake Packages
- Saftronics VG10 – Ratings Efficiency and Watts Loss
- Saftronics VG10 – Standard Specifications
- Saftronics VG10 – DC Link Reactor 100 HP and Above
- Saftronics VG10 – Basic Connection Diagram (Sink Logic, Mainly America)
- Saftronics VG10 – Basic Connection Diagram to PLC (Sink Logic, Mainly America)
- Saftronics VG10 – Basic Connection Diagram (Source Logic, Mainly Europe)
- Saftronics VG10 – Basic Connection Diagram to PLC (Source Logic, Mainly Europe)
- Saftronics PC10 (Obsolete) AC Drives
- Saftronics PC10 – Options & Accessories
- Saftronics PC10 – SF-10 Ethernet Module Kit
- Saftronics PC10 – 24 VDC or 24/120 VAC Input + Relay Option Card
- Saftronics PC10 – 24 VDC or 24/120 VAC Interface Card Kit (PC10, GP10, or VG10 Inverter)
- Saftronics PC10 – Relay Output Card
- Saftronics PC10 – HMI Pump Controller
- Saftronics PC10 – PC10 120 VAC Option Card
- Saftronics PC10 – Palm Pilot Saflink Kit
- Saftronics PC10 – Dynamic Braking
- Saftronics PC10 – Drive Ratings Efficiency and Watts Loss
- Saftronics PC10 – Standard Specifications
- Saftronics PC10 – Part Number: PC102F12-9, PC102F25-9, PC102F50-9 & PC102001-9
- Saftronics PC10 – Part Number: PC102002-9, PC102003-9, PC104F50-9, PC104001-9, PC104002-9 & PC104003-9
- Saftronics PC10 – Part Number: PC102005-9 & PC104005-9
- Saftronics PC10 – Part Number: PC102007-9, PC102010-9, PC104007-9 & PC104010-9
- Saftronics PC10 – NEMA 1 Kit Dimensions
- Saftronics PC10 – Basic Wiring Diagram
- Fincor 5700 Series (Obsolete) AC Drive
- Fincor 5740 Series (Obsolete) AC Drive
- Fincor 5750 Series (Obsolete) AC Drives
- Motortronics Soft Starters
- SOLCON Soft Starters
- SOLCON RVS-DN Digital Soft Starter with Advanced Motor Protection
- Solcon HRVS-DN Digital Soft Starter with Advanced Motor Protection
- Solcon HRVS-TX Digital Transformer Soft Starter
- SOLCON RVS-AX Analog Soft Starters
- SOLCON Solstart Plus Analog Soft Starters
- SOLCON RVS-BX Basic Soft Starter with Built-In Bypass
- SOLCON RVS-DX Digital Soft Starter with Built-In Bypass
- SOLCON RVS-EX Digital Soft Starter for Explosion Proof motors with Built-In Bypass
- SOLCON SEM-N Rugged Soft Starter for Naval and Military Specifications
- SOLCON SOLSTART Miniature Analogue Soft Starter
- SOLCON SOLSTART 1P Single Phase Analogue Soft Starter
- SOLCON SOLBRAKE DC Injection Brake Soft Starter
- Magnetek – Soft Starters
- WEG Variable Frequency Drives, Controls and Motors
- ABB ACS150 Component Drives :: Overview
- DC Variable Speed Drives
- DC Drive Fundamentals
- ABB DCS 400 Digital DC Converter Drive
- ABB DCS 500 DC Drive
- ABB DCS800 DC Drives Overview
- DCS800 – Power Converter Modules
- DCS800 Panel Drive
- DCS800 Enclosed Converters
- DCS800 Rebuild and Upgrade Kits
- Adaptive Programming and Start-up Assistants
- DriveWindow Light – Startup and Maintenance Tool
- DCS800 Commissioning Macros
- DCS800 Firmware
- DCS800 Technical Specifications
- Current Ratings – Modules – Non-Regenerative
- Current Ratings – Modules – Regenerative
- Current Ratings – Modules – DCS800-EP Panel Drive
- DCS800 Dimensions and Weights
- DCS800 Technical Diagram
- DCS800 Plug-in Options
- DCS800 Feedback Options
- DCS800 Communication Options – Fieldbus Control
- DCS800 External Field Supply
- ABB DCS800-EP replaces Reliance FlexPak® 3000 – 230V Drive Cross Reference
- ABB DCS800-EP – 460V Drive Cross Reference
- ABB DCS800-EP – Options Cross Reference
- ABB DCS800-EP – Product Differences and Remedies – Hardware
- ABB DCS800-EP – Product Differences and Remedies – Control/Interface & Features
- ABB DCS800-EP – Drive Dimensions
- ABB DCS800-EP – Installation Procedure – Wiring and Configuration
- ABB DCS800-EP – Parameter Cross-Reference
- FINCOR Series 2600/2610 DC Drives
- 50 Amp & 90 Amp DC Field Regulators
- Mentor II | Quantum III | FXM5 Change of Status
- SIMOREG 6RA24 Siemens DC Drive Features
- SIMOREG 6RA70 Siemens Variable Speed DC Drive Description and Base Drive Catalog Numbers
- SIMOREG 6RA70 Siemens DC Drive Features
- SIMOREG 6RA70 DC Master Design & Operation – Converters
- SIMOREG 6RA70 Design & Operation – Parameterization Devices
- SIMOREG 6RA70 Design & Operation – Software Structure
- SIMOREG 6RA70 Design & Operation – Closed-Loop Functions in Armature Circuit
- SIMOREG 6RA70 Design & Operation – Closed-Loop in Field Circuit
- SIMOREG 6RA70 Design & Operation – Optimization Run
- SIMOREG 6RA70 Design & Operation – Monitoring & Disgnosis
- SIMOREG 6RA70 Design & Operation – Functions of Inputs & Outputs
- SIMOREG 6RA70 Design & Operation – Safety Shutdown (E-STOP)
- SIMOREG 6RA70 Design & Operation – Serial Interface
- 1000 Hp DC Variable Speed Drive System
- 3000 Hp DC Variable Speed Drive
- Permanent Magnet DC Motors
- SCR Drive Controllers (SCR-Silicon Controlled Rectifier)
- Custom Electric Control Panel Shop
- GE AC & DC Motors (G.E. Motors – General Electric AC & DC Motor)
- GE X$D Ultra® NEMA Premium Efficiency – TEFC AC Motors
- GE Kinamatic® Explosion Proof AC Motors
- GE Energy Saver® – TEFC Severe Duty AC Motors
- GE Kinamatic® General Purpose AC Motors
- GE Motors Energy Saver NEMA Premium Efficiency – ODP AC Motors
- GE ValueLine™ EPAct Efficiency – TEFC AC Motors
- GE ValueLine™ EPAct Efficiency – ODP AC Motors
- GE Permanent Magnet Custom DC Motors
- GE ValueLine™ Vertical Hollow Shaft AC Motors
- GE Permanent Magnet Standard DC Motors
- GE ASD Inverter Duty AC Motors
- G.E. Permanent Magnet Washdown DC Motors
- Avtron – Drives, Measurement and Tachs
- Avtron – Adjustable Speed Drives and Drive Systems
- Avtron – Speed and Length Measurement
- Avtron – Tachs, Tachometers, Encoders, Rotary Pulse Generators
- Avtron – Sales Literature and Instruction Sheets
- Avtron – Classic Tach Models
- Avtron – Price Quotation Request Form
- Avtron – Tachometers Availability
- Avtron – Heavy, Mill-Duty Encoders
- Avtron – Setting Air Gap on M285 Sensors
- Avtron – M4 Universal Encoder
- Avtron – M56, M67, M85 THIN-LINE
- Avtron – M285QUAD Outline Drawing
- Avtron – Severe Duty Encoders
- Avtron – Mill-Duty Encoders
- Avtron – M3 Universal Encoder
- Avtron – M3 Applications
- Avtron – M3 Installation
- Avtron – M3 Specifications
- Avtron – Tach Accessories
- Avtron – Tach Solutions
- Avtron – Rugged Environments
- Avtron – Selection by Motor Frame Size
- Avtron – Adapter Kits Outline Drawings
- Avtron – Motors with Brakes
- Avtron – NEMA C Face Mounting
- Avtron – Market Specific Applications
- Dynapar Encoders and Tachs
- ACURO AI25 Encoders
- Acuro Series AI25 Absolute Encoder with DeviceNet Interface
- Acuro Series AI25 Absolute Encoder with Profibus Interface
- Acuro Series AI25 Absolute Encoder with Interbus Interface
- Acuro Series AI25 Absolute Encoder with BiSS Interface
- Acuto Series AI25 Optical Encoders with SSI Interface
- Acuro Series AI25 Absolute Encoder with Parallel Interface
- Acuro Series AD25 Drive Absolute Encoder
- Series R25 – Mill Duty, HOUSED Resolver
- Series 21/22 Heavy Duty Incremetal Encoders
- Series H20 Encoder
- Series HA25 Dynapar Heavy Duty Encoders
- Series HR25 Incremental Encoders
- Series HC25 Incremental Encoders
- Series H58 Heavy Duty Encoders
- Series H42 Heavy Duty Encoders
- Series HA725 Indusrtial Duty Encoders
- Series HD20 Optical Encoder
- Series HD25 Optical Encoder – Harsh Duty
- Series H56 Rotopulser Heavy Duty Encoders
- RIM Tach 6200 Digital Tachometer
- Series X25 Incremental Encoders
- Series 60 Rotopulser Incremental Encoders
- Series H20 Hub Shaft Encoders
- Series HSD25 Harsh Duty Optical Encoders
- Series HSD44
- Series HS20 Sealed Hollow Shaft Encoders
- Series HS35 Sealed Hollow Shaft Encoders
- The NEW HS35R
- Series HSD35 Shaftless Optical Encoder
- Series HSD37 Hollowshaft Rotary Encoder
- Series HSD38 Harsh Duty Optical Encoder
- Series DWD38 Heavy Duty Rotary Encoders
- SLIM Tach HS56 Incremental Encoder / Tachometer
- RIM Tach HS85 Digital Tachometer
- SLIM Tach SL56 Rotary Encoder
- SLIM Tach RL67 Incremental Rotary Encoder
- SLIM Tach SL85 Digital Tachometer
- SLIM Tach SL1250 Incremental Encoder
- RIM Tach 8500 Digital Tachometer
- RIM Tach 1250 Digital Tachometer
- Series R45 Rotopulser Incremental Encoders
- ACURO AI25 Encoders
- Spare Parts and Replacement Parts
- PLC (Programmable Logic Controllers)
- Services
- Projects
- Operator Stations by Joliet Technologies
- AC VFD, AC Controllers and DC VSD by Joliet Technologies
- Material Handling Modernization Project by Joliet Technologies
- 10 DC (SCR) Drive System :: Neptune Marine Oil & Gas
- Mermaid Offshore Services :: 4 DC (SCR) Drive Cabinets
- “Frontier Driller” Offshore Oil Rig :: DC (SCR) Drive Bays
- 1000Hp Siemens SIMOREG 6RA70 DC Variable Speed Drive Retro-Fit
- Smurfit-Stone: Corrugator Crew Sets Production Record
- Steel Slitting Line for Braner USA
- 1000HP DC Drive, Bow Thruster Application for Pegler Automation
- 1000HP DC Traction Motor Drive, Slurry Pump Application for Baker Hughes
- Siemens 6RA70 DC Drive and GE 752 Traction Motor to Hallett Materials
- ABB ACS 800 VFD to Applied Synergistic
- Two 200Hp Variable Speed DC Drives and Motors to JHT Electronics
- Substrate Technology Inc. :: Joliet Technologies, L.L.C.
- Wyco Tool Company
- Variable Frequency Drives and Controls for Food Processing and Bakery Machinery
- Information
- Guide to Harmonics with AC Variable Frequency Drives
- Variable Speed Drives – Application Information
- Reducing harmonics caused by variable speed drives
- FAQ – Variable Speed Drives Frequently Asked Questions
- EASA Electrical Engineering Handbook
- Part Winding Start
- 3Ph Motors, Single Speed
- 3Ph Motors, 2 Speed, Single Winding
- Connections for NEMA DC Motors
- Connections for NEMA DC Generators
- Field Polarities of DC Machines
- Maximum Locked-Rotor Currents – Three-Phase Squirrel Cage Motors
- NEMA Code Letters for AC Motors
- General Speed-Torque Characteristics
- Effect of Voltage unbalance on Motor Performance
- Starting Characteristics of Squirrel Cage Induction Motors
- Allowable Starts and Starting Intervals
- NEMA Size Starters for Three-Phase Motors
- Starter Enclosures
- NEMA Size Starters for Single-Phase Motors
- Determining the Polarization Index of Machine Windings
- Formulas for Electrical Motors
- Motor Application Formulas
- Glossary of Terms
- Variable Frequency Drive (VFD) Case Studies
- VFD Case Studies – ABB drives & motors help to launch lifeboats quickly and safely.
- VFD Case Studies – Paperboard mill benefits from using DC drives
- VFD Case Studies – ABB Drive cuts water pumping bill for semiconductor plant.
- VFD Case Studies – Insulation manufacturing process saves energy with ABB :: Joliet Technologies
- VFD Case Studies – ABB drives cut costs at MINI production plant
- VFD Case Studies – Film maker slashes costs with ABB drives
- VFD Case Studies – ABB drive cuts costs for wooden toy company
- VFD Case Studies – Close pump control doubles efficiency for West of Scotland Water
- VFD Case Studies – ABB Energy Appraisal Saves Money :: Joliet Technologies
- VFD Case Studies – Staggering energy savings prove value of professional audit
- VFD Case Studies – Soft starters save costs for mechanical engineers
- NEMA Frame Chart and T-Frame Chart :: Joliet Technologies
- Model 1681 Instruction Manual – Firing Circuits DC SCR Drives
- IGBT – Insulated Gate Bipolar Transistors :: Joliet Technologies
- Blog
Blog
How to Choose a Custom Plastic Housing Manufacturer?
Choosing a custom plastic housing manufacturer is a practical decision with long-term effects. The supplier may influence product fit, durability, production cost, and launch timing. A small mismatch around a screw boss or cable opening can create delays later. These details are easy to overlook on a first review.
Start with the part’s purpose, operating environment, and expected production volume. Then ask how the manufacturer evaluates materials, wall thickness, tooling, and tolerances. Clear answers matter. Request samples or comparable project examples, and inspect the finish, dimensions, and assembly points closely. A clean-looking prototype is useful, but it does not prove consistent production quality. Ask how defects are recorded and how changes are approved.
Communication deserves the same attention as technical capability. Can the team explain trade-offs in plain language? Will it flag design risks before tooling begins? These questions reveal how the partnership may work under pressure. No checklist catches everything. Even an experienced buyer can miss a detail, so independent design reviews and documented specifications are worth considering. Compare more than quoted prices: include tooling ownership, inspection methods, lead times, and support after production starts. The best fit is not always the largest factory or the lowest bid. It is a manufacturer whose evidence, process, and communication suit the housing and the team behind it. Sometimes the decision remains imperfect; the goal is to understand the risks before committing.
Define Enclosure Protection Needs Using IEC 60529 IP67: 1 m for 30 Minutes
How to Choose a Custom Plastic Housing Manufacturer?
Define Enclosure Protection Needs Using IEC 60529 IP67: 1 m for 30 Minutes
An IP67 rating combines two tests under IEC 60529. The “6” indicates dust-tight protection, while “7” indicates protection against temporary immersion. The immersion test uses defined conditions, commonly up to 1 meter of water for 30 minutes. It does not mean the enclosure is suitable for every wet environment. Deeper water, longer exposure, hot water, or strong water jets may create different risks.
When comparing custom plastic housing manufacturers, ask how they validate the complete assembly. A housing may pass testing with one gasket, screw pattern, or cable entry, then fail after a small design change. Request test details for the actual configuration, including seams, connectors, and mounting features. Check that the material and seal remain suitable for expected temperatures and repeated use. A prototype test is useful, but production consistency matters too. This part is easy to overlook.
Tips: Share the real exposure conditions, not just “waterproof.” Ask for the test method and results, and confirm whether testing covered the finished enclosure. If the housing will face splashing or pressure washing, IP67 alone may not be enough.
IP67 Water-Immersion Reference: 1 m for 30 Minutes
This chart illustrates the IPX7 reference test position for an enclosure less than 850 mm high: its lowest point is 1 m below the water surface for 30 minutes. Test positioning differs for larger enclosures. IP67 also includes dust-tight protection (IP6X); confirm the complete IEC 60529 test requirements and your application conditions with the manufacturer.
Select Resin and Check UL 94 V-0’s 10-Second Afterflame Limit
How to Choose a Custom Plastic Housing Manufacturer? Select Resin and Check UL 94 V-0’s 10-Second Afterflame Limit
Resin selection affects more than flame performance. Consider heat exposure, impact strength, chemical contact, and the housing’s wall thickness. UL 94 V-0 requires each specimen’s afterflame time to stay within 10 seconds after either flame application. The five-specimen test also has a combined afterflame limit. No flaming drops may ignite the cotton below the specimens. Small details matter.
A rated resin does not automatically make every finished housing V-0. Thin ribs, sharp corners, uneven walls, or changes in molding conditions can affect results. Ask the manufacturer to confirm that the proposed material and thickness match the rating, then test representative molded parts. A resin rated at 1.5 mm may not qualify at 1.0 mm. I would also question any claim based only on a similar resin grade; “close enough” is not useful evidence. Request traceable material records and discuss how production checks will catch resin or process changes. It may take another test cycle, but guessing here can cost more later.
Set Part Tolerances with ISO 20457:2018 and Assembly Requirements
ISO 20457:2018 sets a framework for tolerances and acceptance conditions on injection-moulded plastic parts. It does not guarantee that two parts will assemble. Specify nominal dimensions, tolerance limits, and datums on the drawing. Mark function-critical features, such as a connector opening or sealing groove, for tighter control. Broad, unnecessarily tight tolerances can increase cost and scrap risk. Fit is functional. Choose tolerance grades with the manufacturer, considering resin, geometry, tooling, and the molding process.
For a housing, review screw-boss positions, snap-fit arms, gasket lands, and mating-panel clearances together. Use a tolerance stack-up to check the worst-case assembly, not just each part alone. That matters. Define inspection methods, datum setup, and conditioning time. Plastic dimensions can shift with temperature, moisture, and time after molding. Ask for capability data and first-article measurements on critical dimensions before approving production. A trial fit with the actual mating component can reveal issues a drawing misses. Even a careful model can be optimistic. Record agreed exceptions directly on controlled drawings.
Verify Manufacturer Quality Controls Against ISO 9001:2015
A custom plastic housing manufacturer should be able to show how its ISO 9001:2015 quality system works in daily production. Ask for a current certificate and check that its scope covers the site and activities making your parts. The scope matters. A certificate alone does not prove that every housing will meet your drawing.
Request examples of inspection records for incoming resin, molded dimensions, and finished-part appearance. Look closely. Records should identify the part, date, measured result, and responsible operator or inspector. Ask how the team controls mold maintenance and tracks changes to resin, color, or production settings. On a factory visit, compare the written procedure with the actual checks at the machine. They may not match perfectly; that gap deserves a clear explanation.
Ask how the manufacturer handles defects, customer complaints, and corrective actions. A useful response includes containment, cause analysis, and a follow-up check to see whether the fix worked. Review sample traceability records, too: staff should be able to connect a batch of housings to its material and inspection history. I would treat ISO 9001:2015 as a strong process indicator, not a product guarantee. Confirm critical dimensions independently during qualification, especially where a poor fit could disrupt assembly.
Review Tooling, First-Article Results, and Production Capacity Before Approval
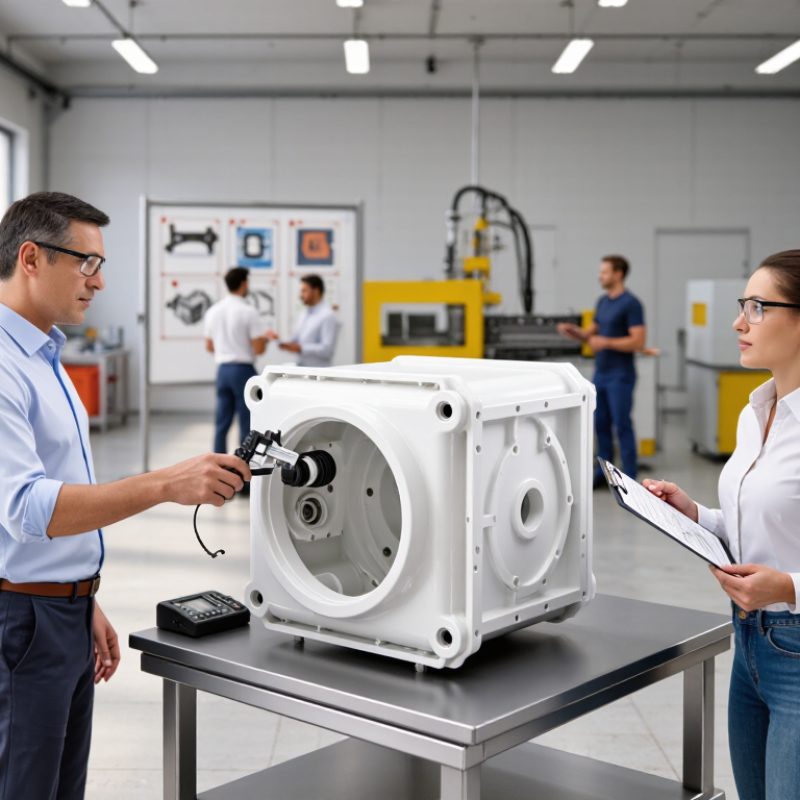
Before approving a custom plastic housing manufacturer, review the tooling plan in detail. Ask how the mold’s parting line, gate location, and cooling channels may affect appearance and dimensions. Confirm who owns the tool and how maintenance or repairs are handled. A glossy sample can hide a weak plan. Small marks matter.
Evaluate first-article results against the actual drawing, not just a photograph. Check critical dimensions, wall thickness, screw-boss fit, and whether the cover closes evenly. Test the part with its intended hardware and cable routing. Record any warping, sink marks, or sharp edges, even if they seem minor. One sample is useful, but it does not prove consistent output.
Before approval, ask for evidence of production capacity: machine availability, expected cycle time, staffing, and inspection frequency. Compare the proposed output with your forecast, including busy periods. A large press alone is not enough. Ask how rejected parts are tracked and what happens if a process drifts. I would leave some uncertainty in the schedule; real production rarely follows a perfect spreadsheet. A small pilot run can reveal gaps before full-volume orders begin.